Injection Mold Base Selection: 24 Configurations Every Mold Engineer Should Know
October 05, 2026
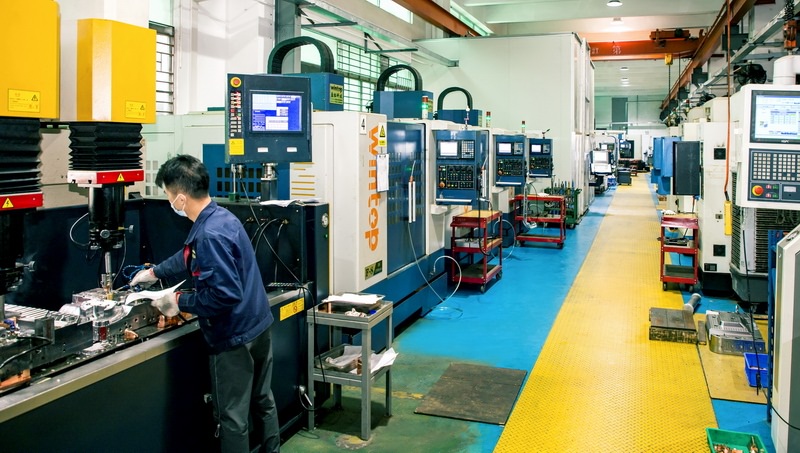
When you're quoting a new injection mold, the mold base decision drives everything downstream — steel cost, machining hours, cycle time, and maintenance access. The classic two-plate (A/B plate) structure remains the workhorse for simple single-cavity or family tools, but it hits a wall once you need runner balancing across 8, 16, or 32 cavities. That's when three-plate tooling earns its keep: the added stripper plate lets you drop a center gate directly over each cavity, eliminating the manual degating step that eats labor on high-volume jobs. The trade-off is roughly 15–25% more steel and a taller stack height, so check your press daylight before committing.
For engineering resins and thin-wall parts, hot runner manifolds and insulated runner systems become the default. A properly zoned hot runner can cut cycle time by 20–30% versus a cold runner on the same part, but you're now budgeting for manifold plates, nozzles, temperature controllers, and the gate-drop alignment tolerances that keep them from leaking. Stack molds and unscrewing molds round out the 24 typical configurations — stack tooling doubles output per cycle but demands precise synchronization of the center parting line, while unscrewing molds for threaded caps need reliable rack-and-pinion or hydraulic drive design from day one.
The practical rule: match the mold base to annual volume, resin, and part geometry — not to what's sitting on the shelf. A 24-configuration reference chart is worth keeping at your desk for quick quoting, but always verify plate thickness, ejector stroke, and locating ring dimensions against your specific press. For more mold sourcing and tooling references, visit MoldWorld at www.moldw.com.